
Down in the lower mechanical room of a busy Broomfield medical office building or multi-tenant commercial plaza, an amber strobe light flashes frantically on the wall. A piercing 90-decibel horn echoes through the basement corridors. The digital control panel on the duplex lift station flashes red: ALARM: HIGH WATER LEVEL — PUMP 1 OVERLOAD TRIP — PUMP 2 RUNNING CONTINUOUS. Over by the sealed cast-iron basin cover, raw sewage is backing up inside the floor drains, threatening thousands of dollars of server racks, medical records, and finished drywall.
Your sewage grinder pump system is jammed.
Don’t ignore the high-water horn or simply press “Silence” and walk away.
When a commercial grinder pump stops grinding, raw municipal solids and wastewater don’t magically disappear. Every flush from the floors above adds dynamic head to an already overflowing wet well. Within thirty minutes, contaminated blackwater will breach floor drains and basement toilet bowls.
Commercial sewage grinder pumps are high-torque industrial machines designed to pulverize sanitary solids into a slurry and pump them uphill against steep dynamic head pressures. But when industrial rags, non-woven polypropylene “flushable” wipes, dental floss nests, or construction debris wedge between the high-chrome cutter teeth, the motor pulls locked-rotor amps (LRA) in milliseconds. Thermal overloads trip.
Let’s examine the mechanical physics of commercial grinder pumps, dissect radial cutter clearance tolerances, troubleshoot float switch grease blinding, and review master plumber emergency rebuild and panel diagnostic protocols.
1. Grinder Pump Anatomy: Cutter Discs, Shredder Rings & Hydraulic Impellers
How does a commercial grinder pump differ from a standard residential sewage ejector?
A traditional sewage ejector uses a semi-open vortex impeller to pass solid spherical objects up to 2 inches in diameter through large 2″ or 3″ discharge piping. Ejectors don’t chop solids; they simply swirl them through the volute.
A commercial grinder pump operates under a completely different hydraulic philosophy. Grinder pumps are engineered to tackle high dynamic heads (often 50 to 130+ feet of vertical lift) through smaller 1-1/4″ to 2″ pressurized force mains. To prevent smaller force mains from plugging, the pump must pulverize everything into a fine, liquid slurry before the fluid enters the impeller eye.
The Two-Stage Cutting Mechanism
At the bottom of the submersible pump volute sits a hardened cutting assembly crafted from 440C stainless steel or Rockwell C 58-60 hardened high-chrome alloy:
- The Stationary Cutter Ring (Shredder Ring): Bolted solidly to the pump suction inlet. It features a perimeter of machined, razor-sharp shearing slots and internal cutting edges.
- The Rotating Cutter Blade (Impeller Cutter): Mounted directly to the hardened stainless steel motor shaft, spinning at either **1,750 RPM or 3,450 RPM**. As it rotates, it sweeps past the stationary ring with scissor-like shearing action, delivering tens of thousands of cutting strokes per minute.
The Critical .008″ Cutter Clearance
For a grinder pump to shred synthetic wipes, feminine hygiene products, and latex gloves without jamming, the mechanical gap between the spinning cutter and stationary shredder ring must remain microscopic:
Think about that clearance. Eight-thousandths of an inch is barely thicker than two sheets of notebook paper.
When sand, abrasive grit, or construction grout passes through the cutter, the hardened cutting edges round off. Worse yet, if fine textile fibers wedge into the gap, they deflect the cutter blade axially. The gap expands from 0.008″ to 0.020″.
Once clearance opens up, the pump stops cutting. Fibers stop shearing and begin wrapping tightly around the rotating shaft like a winch cable. The cutter binds against the stationary ring.
2. Electrical Diagnostics: Locked-Rotor Amperage (LRA) & Thermal Lockout
What happens electrically when a shredder jams?
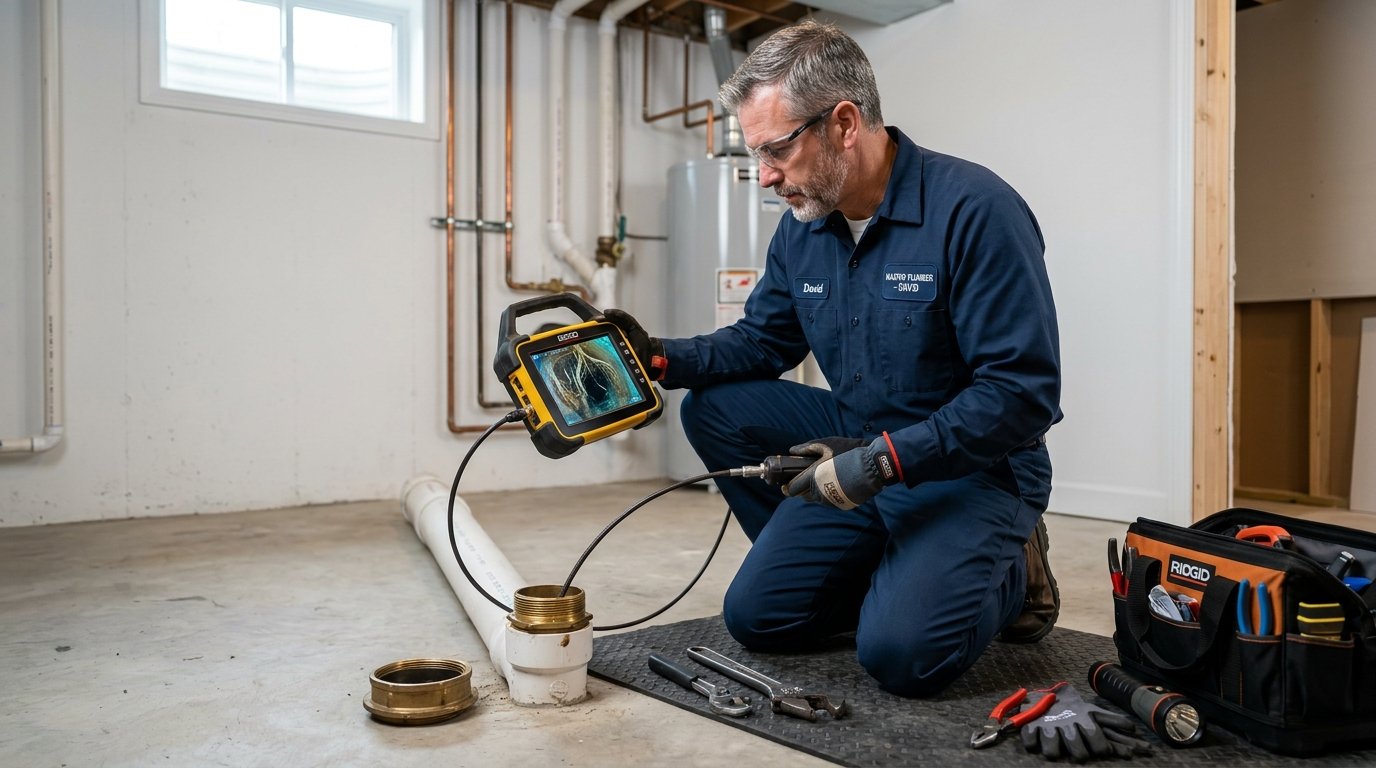
Electric induction motors draw a specific full-load amperage (FLA) when pumping liquid under standard design conditions. But when the cutter mechanism suddenly binds solid, the motor rotor is instantly locked in place while full line voltage remains applied across the stator windings.
In that instant, the motor draws **Locked-Rotor Amps (LRA)**:
| Motor Rating | Supply Voltage & Phase | Normal Full Load Amps (FLA) | Locked Rotor Amps (LRA) | Time to Thermal Overload Trip |
|---|---|---|---|---|
| 2.0 HP Grinder | 208V / 1-Phase | 13.5 A | 68.0 A | 3 to 7 Seconds |
| 2.0 HP Grinder | 240V / 1-Phase | 12.0 A | 60.0 A | 3 to 7 Seconds |
| 3.0 HP Grinder | 208V / 3-Phase | 9.8 A | 54.0 A | 4 to 8 Seconds |
| 5.0 HP Grinder | 480V / 3-Phase | 7.6 A | 45.0 A | 3 to 6 Seconds |
When 60+ amps course through copper motor windings rated for 12 amps, resistance heating ($I^2 R$) generates extreme temperatures. In less than eight seconds, winding temperatures climb toward 300°F.
To prevent the motor from bursting into flames inside the oil-filled housing, the manufacturer builds in an internal thermal overload switch or wires an external bimetallic thermal protector into the control panel circuit. The overload contacts snap open, de-energizing the motor magnetic contactor.
The pump goes dead. The alarm illuminates.
3. Single-Stage vs. Two-Stage Grinder Mechanisms
In commercial wastewater engineering, pumps utilize distinct cutter architectures tailored to the anticipated solid waste stream:
| Feature | Radial Cutter Design (e.g., Barnes Razor / Myers VR) | Axial Cutter Design (e.g., Flygt M3000 / Zoeller Shark) |
|---|---|---|
| Cutter Motion | Spinning horizontal disc sweeping past radial shear slots. | Heavy conical rotating head with spiral teeth boring into stationary cutter ring. |
| Cutting Force | High-speed shearing scissor action (3,450 RPM). | Crushing and masticating axial extrusion action (1,750 or 3,450 RPM). |
| Tolerance to Non-Woven Textiles | Exceptional when clearance is strictly maintained at 0.008″. | Better at passing heavy plastics, clothing fragments, and rubber gloves. |
| Wear Adjustment | Shims behind rotating cutter blade. Requires feeler gauge. | Axial adjustment screw on bottom casing without pump teardown. |
4. Duplex Control Panel Anatomy: Alternators, Capacitors & Float Failures
Commercial facilities almost never rely on a single grinder pump. The International Plumbing Code (IPC Section 712.4.2) requires commercial lift stations receiving waste from six or more plumbing fixtures to incorporate a duplex pump arrangement.
How the Duplex Brain Functions
Inside the NEMA 4X fiberglass control panel enclosure, an electronic alternator logic board coordinates the two pumps:
- Cycle 1: Pump 1 starts, empties the basin down to the “Stop” level, and turns off.
- Cycle 2: Next inflow cycle, the alternator flips. Pump 2 starts, empties the basin, and turns off.
- High Inflow / Jam Condition: If Pump 1 is running but cannot keep up (or if Pump 1 tripped on thermal overload), the liquid continues to rise until it triggers the “Lag / High-Water” float switch. The panel immediately energizes Pump 2 to assist, while latching the visual and audible emergency alarm circuits.
The Enemy: Grease Crust & Float Blinding
Why do float switches fail along the Colorado Front Range?
Commercial wastewater contains animal fats, vegetable oils, and synthetic soap curds. Over months of operation, this grease emulsifies, floats to the surface of the wet well, and cools into a dense, buoyant crust resembling hardened tallow.
Suspended mechanical float switches become encrusted in this grease cake:
- Float Weighed Down: A 10-pound mass of grease clings to the “Start” float, preventing its internal steel ball from rolling across the electrical contacts when water rises. The pump never receives the signal to turn on.
- Float Glued in the Up Position: Grease wedges the “Stop” float against the basin wall, holding it tipped upward. The grinder pump continues running dry long after the basin is pumped empty. Submersible pumps rely on wastewater for motor cooling; run a dry grinder pump for fifteen minutes, and the mechanical silicon-carbide shaft seals shatter from thermal shock.
5. Cold Weather Lift Station Hazards: Frozen Force Mains
In Broomfield and across the Denver metro area, our winter frost line extends to **36 to 42 inches below grade**.
When a grinder pump discharges into an exterior force main running under an uninsulated parking lot or through an unheated retaining wall, standing water in the discharge riser will freeze solid overnight if the check valve fails or if the line was graded without proper continuous drainage slope.
If the discharge pipe freezes solid with ice, the grinder pump turns on against a dead-headed hydraulic block. The spinning impeller churns the same three gallons of water trapped in the volute. In minutes, that trapped water boils into steam, melting the PVC discharge piping, de-tempering the cutting blades, and frying the pump stator.
6. Master Plumber Emergency Diagnostics: Step-by-Step Restoration Protocol
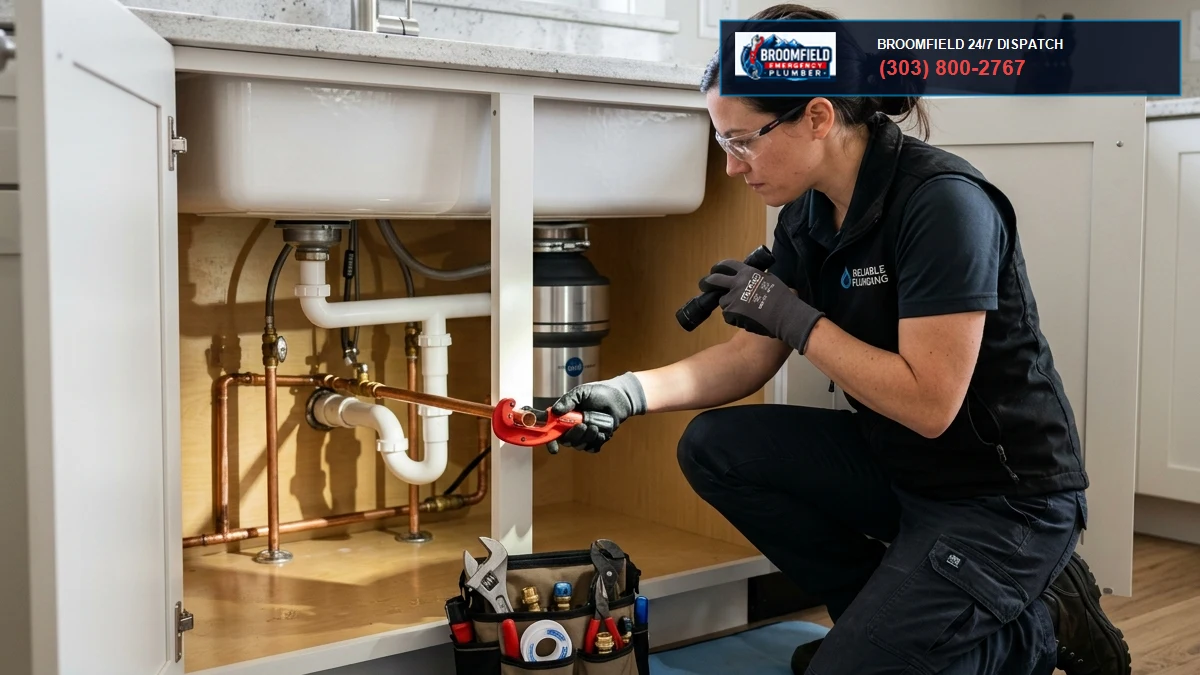
When our commercial emergency trucks arrive at a flashing lift station alarm, we execute a rigorous forensic restoration sequence:
| Diagnostic Sequence | Field Test Procedure | Normal Tolerance | Emergency Action if Out of Spec |
|---|---|---|---|
| 1. Lockout / Tagout (LOTO) | Disconnect primary 208V/240V/480V three-phase disconnect at the panel. | Zero voltage verified with Fluke CAT-IV multimeter. | Never insert hands or tools into a grinder basin without physical mechanical disconnect and LOTO lock applied. |
| 2. Motor Winding Resistance | Measure resistance across T1-T2, T2-T3, T1-T3 with digital ohmmeter. | Balanced resistance within ±3% across all three phases (typically 1.5 to 8.0 Ω). | Infinite resistance (∞) indicates open winding. Zero resistance indicates shorted coil. Pull pump for full stator rewind or replacement. |
| 3. Megohmmeter (Megger) Insulation Test | Apply 500V or 1,000V DC between motor leads and ground wire. | > 20 Megaohms (MΩ) for installed pumps; > 100 MΩ for new. | Reading below 1.0 MΩ confirms water ingress past the mechanical shaft seal into the oil chamber. Overhaul required. |
| 4. Mechanical Jam Extraction | Fit a hardened spanner wrench or hex drive to the external shaft cutter bolt. Manually rotate counter-clockwise. | Smooth, free 360-degree rotation with light hand torque. | If seized solid, extract foreign debris (textiles, cable ties, mop strings) with heavy needle-nose pliers. Reset cutter clearance to 0.008″. |
| 5. Float Switch Tilt Verification | Manually lift floats one by one with an insulated fiberglass reach rod. | Audible click inside float; control panel relay clicks; pump contactor pulls in immediately. | Scrape grease cake using hot-water pressure wash. Replace failed mechanical microswitches with sealed transducer or optical sensors. |
7. Sizing Calculations: Total Dynamic Head (TDH) & Hazen-Williams Losses
A frequent cause of premature grinder pump failure is hydraulic misapplication: installing a pump that operates off the right-hand end of its pump curve where motor amperage runs continuously high.
To ensure the replacement pump operates inside its hydraulic sweet spot, calculate Total Dynamic Head ($TDH$):
Where:
- $H_{\text{static}}$ = Vertical elevation difference from basin bottom to highest discharge point (ft)
- $H_{\text{friction}}$ = Pipe wall friction loss calculated via Hazen-Williams formula:
$$h_f = 0.2083 \times \left(\frac{100}{C}\right)^{1.852} \times \frac{Q^{1.852}}{d^{4.8655}} \times L$$ - $H_{\text{fittings}}$ = Equivalent pipe length losses through check valves, 90° elbows, and gate valves (ft)
- $P_{\text{residual}}$ = Pressure required to discharge into pressurized city force main (ft of head = PSI × 2.31)
If a facility has 38 feet of static lift and 18 feet of friction loss across 350 feet of 2″ schedule 40 PVC ($TDH = 56\text{ ft}$), installing a pump rated for a maximum cutoff head of 50 feet will result in continuous zero-flow operation, severe overheating, and instant motor burnout.
8. Confined Space Safety: OSHA & NFPA 820 Wastewater Regulations
Entering a commercial sewage wet well is classified under OSHA Standard 1910.146 as a Permit-Required Confined Space.
Anaerobic decomposition inside commercial sewage pits generates lethal atmospheric hazards:
- Hydrogen Sulfide ($H_2S$): Heavier than air. Paralyzes olfactory nerves at 100 PPM. Lethal at 300 PPM in minutes.
- Methane ($CH_4$): Highly explosive hydrocarbon gas with a Lower Explosive Limit (LEL) of 5%.
- Oxygen Depletion ($O_2$): Bacterial consumption drives ambient oxygen levels below 19.5%, causing sudden asphyxiation.
Our commercial crews utilize calibrated 4-gas atmospheric monitors, forced mechanical ventilation blowers (minimum 2,000 CFM), full-body harness retrieval tripods, and explosion-proof non-sparking hand tools meeting NFPA 820 Class 1, Division 1 electrical classifications. Never enter a sewage wet well without certified confined-space safety protocols.
9. Real-World Case Study: Broomfield Office Plaza Basement Flooding Averted
In January 2026, an alarm sounded at 6:15 AM at a commercial professional center on 120th Avenue in Broomfield. The lower-level accounting firm was thirty minutes from opening, and their floor sinks were gurgling contaminated wastewater.
Our emergency commercial truck arrived within 25 minutes. Here is what we found:
- Control Panel State: Pump 1 thermal overload tripped. Pump 2 starter contactor chattering rapidly due to pitted silver contacts. Wet well water level stood three inches below the electrical conduit entry.
- Pump Extraction: We hoisted Pump 1 using the stainless steel guide rail crane. The cutter teeth were choked with an 8-inch solid rope of microfiber mop strands and synthetic disinfectant wipes flushed by the night janitorial crew.
- Field Rebuild: We torqued the shaft reverse bolt, extracted the bound textile nest, measured cutter gap at 0.019″ (nearly double tolerance), removed two brass adjustment shims to restore clearance to 0.008″, and meggered the motor at 85 Megaohms (healthy stator insulation).
- Restoration: We replaced the chattering control panel contactor, steam-cleaned the blinded float switches, and ran three automated alternation pump cycles. The wet well emptied cleanly in 42 seconds per cycle. Zero water escaped onto the carpet.
10. Guide-Rail Disconnect Systems: Why Manual Basin Entry is Obsolete
In modern commercial architecture, nobody should ever have to unbolt a pump at the bottom of a wastewater pit.
The International Plumbing Code and best trade practices dictate dual-pipe guide rail quick-disconnect systems:
- Cast Iron Discharge Foot: Bolted permanently to the concrete basin floor and connected to the discharge force main.
- Mating Slide Flange: Bolted to the pump discharge neck with an integrated NBR or Viton seal face.
- Stainless Steel Guide Pipes: Two vertical 304 or 316 stainless steel pipes extend from the discharge foot up to the access hatch.
When the pump is lowered on a stainless lifting chain, gravity guides the slide flange down the rails until it mates tightly against the discharge foot. Hydrostatic discharge pressure locks the elastomeric seal bubble-tight. When service is required, the pump is hoisted straight up to ground level without loosening a single bolt inside the pit.
11. Preventive Maintenance Checklist: Keeping Grinder Systems Jam-Free
To prevent a sudden loss of building drainage and costly blackwater cleanups:
- Monthly Float Visual Inspection: Check float switch freedom. Wash away grease buildup with hot water wand.
- Quarterly Current Draw Logging: Record running amperage of both pumps under full load. Any rise above 10% of FLA indicates cutter dulling or hydraulic restriction.
- Semi-Annual Oil Chamber Check: Drain sample plug on pump motor housing. Clear oil indicates healthy seals. Milky or cloudy oil indicates water emulsion and requires immediate mechanical seal renewal.
- Annual Feeler Gauge Recalibration: Hoist pumps to surface. Inspect cutting edges under 10x magnification. Reset clearance to 0.008″ using factory shims.
12. Commercial Lease Language & Tenant Plumbing Rules
The most engineered grinder pump in the world will fail if occupants treat toilets like trash cans.
We strongly advise commercial building landlords to insert explicit wastewater rider clauses into tenant lease agreements:
“Tenants shall strictly prohibit the disposal of non-flushable sanitary wipes, paper towels, dental floss, mop strands, latex gloves, and grease into plumbing fixtures. Any pump jam or wet well overflow directly traced to prohibited tenant waste shall be billed 100% to the offending tenant’s common area maintenance (CAM) account.”
Posting clear, laminated instructional signage in commercial restrooms reduces wipe-induced grinder jams by over 75% overnight.
13. Wet Well Hydraulic Sizing Math: Cycle Frequency & Retention Margins
Why do commercial grinder wet wells overflow so rapidly during peak usage?
In commercial buildings, basin volume cannot simply be guessed. Wet wells must be sized according to peak fixture units and allowable motor starts per hour. Submersible motor manufacturers strictly specify a maximum of **10 to 12 starts per hour** to prevent thermal degradation of motor insulation.
To determine minimum active liquid storage volume ($V_{\text{active}}$) in gallons between the “Pump Stop” and “Pump Start” float levels:
Where:
- $T_{\text{cycle}}$ = Minimum allowable cycle time in minutes ($T_{\text{cycle}} = \frac{60\text{ min}}{\text{Max Starts/hr}} = \frac{60}{10} = 6\text{ minutes}$)
- $Q_{\text{pump}}$ = Rated flow rate of a single grinder pump in GPM (e.g., 40 GPM at 60 ft TDH)
Across a standard 36-inch diameter cylindrical fiberglass basin, one vertical inch of depth contains:
To achieve 60 gallons of active storage, the vertical differential between the “Stop” and “Lead Start” float must measure at least **13.6 inches**. If an inexperienced contractor hangs the floats only 4 inches apart, the pump will cycle every 90 seconds, pulling heavy inrush current 40 times per hour until the thermal protector permanently welds shut.
14. Soft Starters vs. Across-The-Line Contactor Dynamics
When a 3-horsepower or 5-horsepower grinder pump kicks on, the electrical and mechanical systems experience a violent jolt.
In traditional Across-the-Line (DOL) starters, full supply line voltage (208V, 240V, or 480V) is slammed across the motor stator in zero milliseconds. The motor produces an explosive torque surge:
- Mechanical shock twists the pump volute on its guide rail base.
- Starting current spikes to 600% of full-load amperage, dimming lights across the facility.
- Internal radial cutter teeth slap against solids with violent impact, increasing risk of tooth chipping.
In modern Front Range commercial facilities, master plumbers upgrade control panels with Solid-State Soft Starters (SSMS). Soft starters use silicon-controlled rectifiers (SCRs) to ramp motor voltage smoothly over 1.5 to 2.5 seconds:
- Starting current is clamped to a manageable 250% to 300% of FLA.
- Torsional stress on the stainless steel motor shaft is reduced by over 70%.
- The radial cutter blade accelerates smoothly into the waste stream, slicing through wipes without torque spikes that cause false thermal overload trips.
15. Check Valve Slap, Water Hammer & Force Main Anti-Air-Lock Physics
What causes the terrifying metallic clang heard every time a sewage grinder pump stops?
When the pump de-energizes, the column of wastewater in the vertical force main abruptly reverses direction under gravity, slamming the heavy swing check valve disc into its brass or cast iron seat. This is check valve slam.
To protect piping from fatigue cracks:
- Install Resilient-Hinged Ball Check Valves: Replace rigid swing flappers with vulcanized rubber ball check valves. The rubber-encapsulated hollow ball is pushed upward during flow and sinks softly into a conical elastomer seat when flow ceases, eliminating 95% of hydraulic shock.
- Drill the 3/16″ Anti-Airlock Relief Hole: The International Plumbing Code requires a 3/16-inch weep hole drilled into the discharge pipe between the pump volute outlet and the check valve. When the wet well is pumped down, trapped air can compress under the check valve, preventing water from reaching the impeller eye during the next cycle (air-locking). The 3/16″ hole allows trapped air to vent freely into the basin, guaranteeing instant hydraulic prime.
16. Emergency Backup Power & Generator Load Step Sizing
What happens to your below-grade lift station when a violent Front Range winter storm knocks out commercial utility power across Broomfield?
Plumbing fixtures on the upper floors of an office tower or medical center will continue to be flushed by occupants during a blackout. If the duplex grinder lift station does not transfer seamlessly to emergency standby power, the wet well will fill and overflow within forty-five minutes.
Under NFPA 110 (Standard for Emergency and Standby Power Systems) and commercial building codes, lift station circuits connected to automatic transfer switches (ATS) must be engineered for motor locked-rotor starting kVA:
- Starting kVA Sizing: A 3 HP 208V single-phase grinder pump requires roughly 3.5 kW of running power, but demands over 14 kVA of instantaneous starting capacity. If the emergency generator is undersized, the starting voltage dip will exceed 20%, causing the ATS contactors to chatter or drop out.
- Staggered Restart Logic: Duplex control panels connected to backup generators must incorporate time-delay relays (typically 10 to 15 seconds) preventing both grinder pumps from attempting to start simultaneously when generator power first energizes the bus.
Frequently Asked Questions About Commercial Sewage Grinder Pumps
Why is my commercial grinder pump running continuously without shutting off?
A continuously running pump is usually caused by one of three issues: a stuck or grease-weighted ‘Stop’ float switch holding the circuit closed, a severe mechanical cutter jam that sheared the drive key (motor spins but cutter doesn’t turn), or a clogged discharge check valve that prevents wastewater from leaving the basin.
Can you flush ‘flushable wipes’ into a commercial grinder pump system?
Absolutely not. So-called ‘flushable’ wipes are composed of woven synthetic polyester and polypropylene fibers that do not break down in water. In commercial high-volume environments, these fibers twist into dense ropes that wedge into the 0.008\” cutter gap, seizing the motor and causing thermal overload trips.
What does it mean when the lift station high-water alarm sounds?
It means the liquid level inside the wet well has risen past the normal operating pump-start level and triggered the emergency high-water float. This signals that neither pump is operating, the pumps are failing to keep up with inflow, or the discharge force main is blocked.
How long can a commercial building operate once a grinder pump fails?
Very briefly. Depending on wet well basin volume and building occupancy, an un-pumped commercial basin typically fills to overflowing within 20 to 45 minutes of active plumbing fixture use. Fixture usage must be halted immediately until service arrives.
Who provides 24/7 commercial sewage grinder pump repair in Broomfield, Colorado?
Broomfield Emergency Plumber provides 24/7 commercial lift station and grinder pump emergency dispatch across Broomfield, Boulder, and the Denver metro area. Call our master plumbers immediately at (303) 647-3363 for pump pulls, cutter rebuilds, and control panel diagnostics.
Sewage Grinder Alarm Sounding or Lift Station Backing Up?
Don’t let a sewage pump failure flood your commercial property with hazardous blackwater. Our master commercial plumbers carry heavy-duty replacement grinder pumps, control panel components, and guide-rail hoists ready for immediate 24/7 dispatch.
Call (303) 647-3363 for 24/7 Emergency Grinder Pump Dispatch